Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
Whatsapp
Precision-engineered oil and air filter kits designed for agricultural machinery and heavy equipment — ensuring clean cabin environments and peak engine performance.
In modern agricultural machinery, commercial vehicles, and heavy industrial equipment, the term "oil filter for cabin air purification" refers to a specialized category of filtration components that serve a dual purpose: maintaining the cleanliness of engine oil and hydraulic fluids while simultaneously contributing to the overall air quality within the operator's cabin. As equipment cabins become increasingly sealed and operator health standards rise globally, the role of integrated filtration systems — including oil filters, cabin air filters, and combined filter kits — has expanded well beyond simple mechanical maintenance.
The AL115625 AL177185 Air Filter Kit for John Deere 6105M-6140M series is a prime example of how modern filter kits are engineered to meet both engine protection and cabin environment standards simultaneously. These kits combine primary and secondary filtration stages to capture dust, pollen, exhaust particulates, and microscopic contaminants that would otherwise degrade both the engine's performance and the operator's breathing environment inside the cab.
Modern oil and air filter kits protect not only the mechanical components of heavy machinery but also safeguard the operator's respiratory health — a critical compliance requirement in global occupational safety standards including OSHA, EU Machinery Directive, and ISO 23875.
The global market for cabin air filtration and oil filtration systems in off-highway and heavy-duty vehicles is experiencing robust growth. According to industry analysts, the off-highway filtration market is projected to exceed USD 8.5 billion by 2028, driven by tightening emissions regulations, increasing mechanization in agriculture across Asia-Pacific, and the rapid expansion of mining and construction activities in emerging economies.
In China alone, the agricultural machinery sector has undergone a dramatic transformation over the past decade. With over 230 million hectares of farmland under mechanized cultivation, the demand for reliable, high-performance filter components — including oil filters designed to support cabin air purification — has surged significantly. Manufacturers and parts suppliers that can offer full-category, full-scenario coverage are increasingly valued as strategic partners rather than simple commodity vendors.
Commercial vehicle fleets — including long-haul trucks, urban buses, and construction vehicles — represent another major segment. Fleet operators are under increasing pressure from both regulatory bodies and corporate ESG commitments to ensure driver wellbeing, reduce maintenance downtime, and extend vehicle operational life. Oil filters that integrate with cabin air management systems directly address all three priorities.
The connection between oil filtration and cabin air quality is more direct than many operators realize. In heavy machinery and agricultural tractors, engine blow-by gases — which contain vaporized oil, combustion byproducts, and fine particulate matter — can infiltrate the cabin's HVAC intake if the engine's positive crankcase ventilation (PCV) and oil filtration systems are not functioning optimally. A degraded or clogged oil filter allows contaminated oil to circulate through the engine, increasing the generation of these harmful gases and accelerating the contamination of cabin air filters downstream.
Furthermore, hydraulic system oil filters in agricultural equipment and mining machinery directly affect the cleanliness of hydraulic fluid. Contaminated hydraulic fluid can cause micro-leaks and seal degradation, releasing fine oil mist into enclosed engine compartments — and eventually into the operator's cabin. Maintaining high-efficiency oil filtration is therefore a foundational step in any comprehensive cabin air purification strategy.
The filtration industry is undergoing rapid transformation driven by electrification, digitalization, and stricter environmental standards.
Next-generation filter media incorporating nano-fiber layers achieve sub-micron particle capture efficiency exceeding 99.97%, dramatically improving both oil cleanliness and cabin air quality in agricultural and mining environments.
Embedded pressure differential sensors and IoT connectivity allow fleet managers to monitor filter condition in real time, triggering predictive maintenance alerts before filter degradation impacts cabin air quality or engine performance.
Combining traditional mechanical oil filtration with electrostatic precipitation technology enables the capture of sub-micron oil aerosols and combustion particles that conventional filters cannot retain, setting a new standard for cabin air purity.
Driven by sustainability mandates, manufacturers are developing biodegradable filter housings and extended-service-interval media that reduce waste while maintaining superior filtration performance across longer operational cycles.
AI-powered oil analysis platforms can now predict filter replacement intervals with high accuracy by analyzing oil contamination patterns, reducing unnecessary replacements and ensuring cabin air systems always operate with clean, effective filters.
Chinese manufacturers like Huanyang Juchuang are closing the technology gap with international brands, offering OEM-equivalent or superior filtration performance at competitive price points — accelerating adoption across Asia-Pacific markets.
Oil filters for cabin air purification are deployed across a diverse range of industrial and commercial environments, each with unique filtration demands.
Operators of large agricultural tractors such as the John Deere 6105M-6140M series work in environments with extreme dust, crop residue, and pesticide aerosols. High-efficiency oil filter kits combined with cabin air filters prevent these contaminants from entering the engine oil circuit and the operator's breathing zone, protecting both the machine and the human. Extended-interval filter kits are particularly valued during peak harvest seasons when downtime is unacceptable.
Open-pit mining environments generate silica dust, diesel exhaust particulates, and chemical fumes at concentrations far exceeding urban environments. Oil filters in mining dump trucks must handle extreme thermal cycling and heavy contamination loads. Cabin air purification in these machines is a direct occupational health requirement, with regulatory bodies mandating specific air quality standards inside operator cabs. Integrated filtration solutions that address both hydraulic oil cleanliness and cabin air quality are essential in this sector.
Bus operators face dual pressures: passenger air quality regulations and driver health standards. Engine oil contamination from degraded oil filters accelerates the generation of blow-by gases that can infiltrate the vehicle's HVAC system. Modern bus fleets are increasingly specifying combined oil and cabin air filter service intervals as part of a unified air quality management protocol, reducing driver sick days and improving passenger experience.
Wheel loaders, graders, and compactors operate in construction zones where concrete dust, bitumen fumes, and diesel exhaust create complex contamination mixtures. Oil filters that maintain hydraulic fluid cleanliness directly reduce the frequency of hydraulic seal failures, which are a primary source of oil mist contamination within enclosed equipment cabs. Proactive oil filtration is increasingly recognized as a cabin air quality control measure in this sector.
Forestry harvesters and specialty crop equipment operate in high-humidity, high-organic-matter environments where bio-contamination of engine oil is a significant risk. Oil filters with antimicrobial media and enhanced water-separation capabilities are increasingly specified for these applications, simultaneously protecting engine components and preventing mold-contaminated air from entering operator cabins.
As the heavy equipment industry transitions toward hybrid powertrains, the role of oil filtration evolves. Hybrid systems generate unique contamination profiles in their lubrication circuits, requiring advanced filter media capable of handling both conventional combustion byproducts and new contaminants from electric motor cooling fluids. Cabin air purification in these next-generation machines benefits directly from advances in integrated filtration system design.
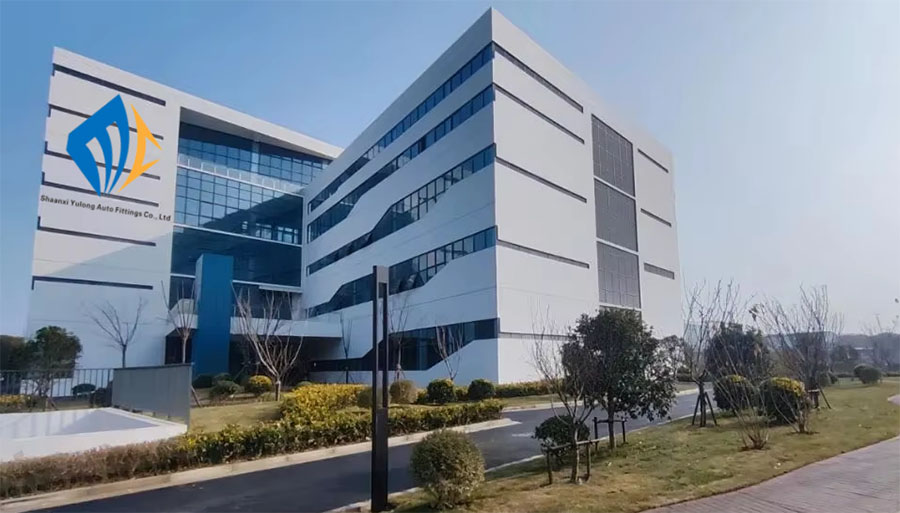
Huanyang Juchuang (Shaanxi) Technology Equipment Co., Ltd. is a professional and highly competitive leading enterprise in the field of parts for buses, agricultural machinery, commercial vehicles and mining equipment. With years of in-depth cultivation in the industry, we have always adhered to the core philosophy of "Professionalism Builds Quality, Innovation Leads the Future".
Since its establishment, the company has adhered to the principles of honest operation and pragmatic practice. Relying on profound industry accumulation, mature technical strength and a complete service system, it has won high recognition and trust from customers in 32 provinces, autonomous regions and municipalities directly under the Central Government of China.
We have gradually developed into a comprehensive parts service provider integrating R&D, production, integrated supply and sales — currently the only professional service provider in China that has achieved full-category and full-scenario parts coverage.
Full-spectrum parts R&D, production, supply and service across four major industrial fields.
The company focuses on the R&D, production, integrated supply and sales of parts in four major fields: buses, agricultural machinery, commercial vehicles and mining equipment. Its core business covers the customized R&D, standardized production, batch supply and supporting services of various core equipment parts and general parts, fully meeting the parts needs for maintenance, upkeep and upgrading of equipment.
Our product system is rich and complete, covering all categories and scenarios from core transmission components and braking components to general electrical accessories and structural parts. Relying on a professional technical team, we provide timely, customized and one-stop overall parts solutions for mining dump truck and heavy equipment users, solving the pain points of scattered parts procurement, poor adaptability and delayed supply.
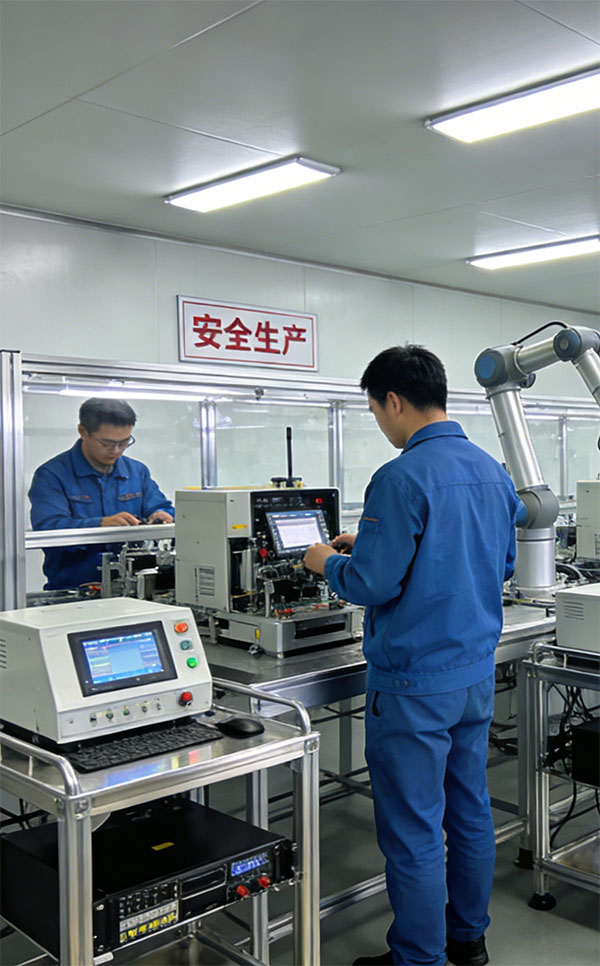
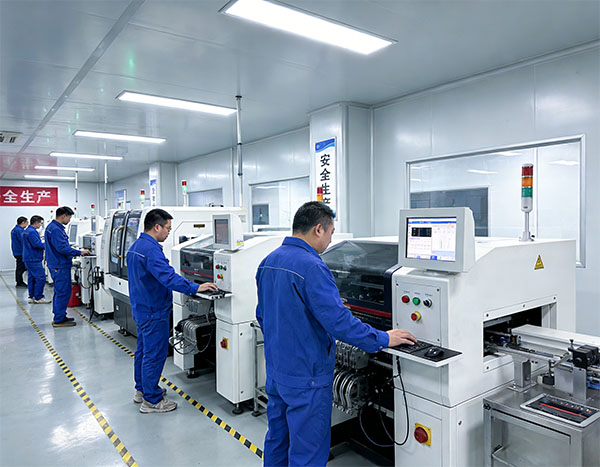
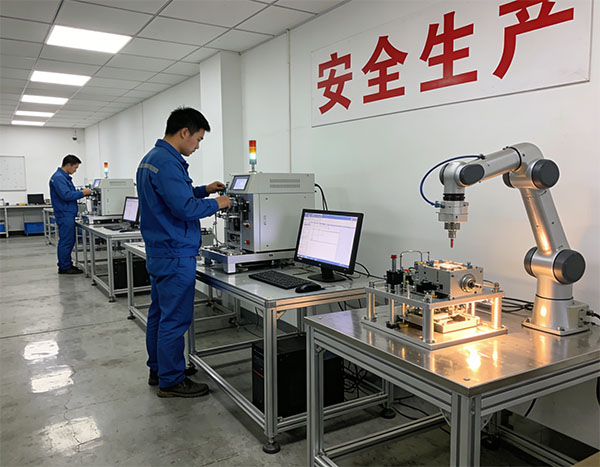
The company started in the field of equipment parts trade. With accurate industry insight and honest business philosophy, it quickly opened up the domestic market. With the upgrading of market demand, we gradually expanded business boundaries, set up a professional R&D team, invested in production line construction, and realized the transformation to an integrated "R&D, production + trade and service" enterprise — becoming the only professional service provider in China achieving full-category and full-scenario parts coverage.
In the process of development, we have always adhered to the parallel development of technological innovation and service upgrading, continuously optimized the product system, improved the supply chain layout, and gradually expanded coverage to all 32 provinces, autonomous regions and municipalities directly under the Central Government of China.
In the future, the company will continue to deepen its focus on core fields, expand product application scenarios, promote technological iteration and upgrading, and steadily move towards the goal of "building a leading domestic and internationally renowned equipment parts service provider".
Corporate culture is the core driving force for enterprise development — integrating integrity, professionalism, innovation and win-win into every link of our operations.
Integrity as the foundation, professionalism as the cornerstone, innovation for the future, and win-win coexistence
Empower equipment upgrading with high-quality parts, assist customer development with professional services, and promote high-quality progress of the industry
Become a benchmark enterprise in China's equipment parts industry and build a sustainable and win-win industrial ecosystem
Pragmatic practice, striving for excellence, forging ahead with determination, and climbing new heights
We have always adhered to the service concept of "Customer First", putting customer needs first, winning trust with integrity, solving problems with professionalism, breaking through development with innovation, and achieving long-term development with win-win results.
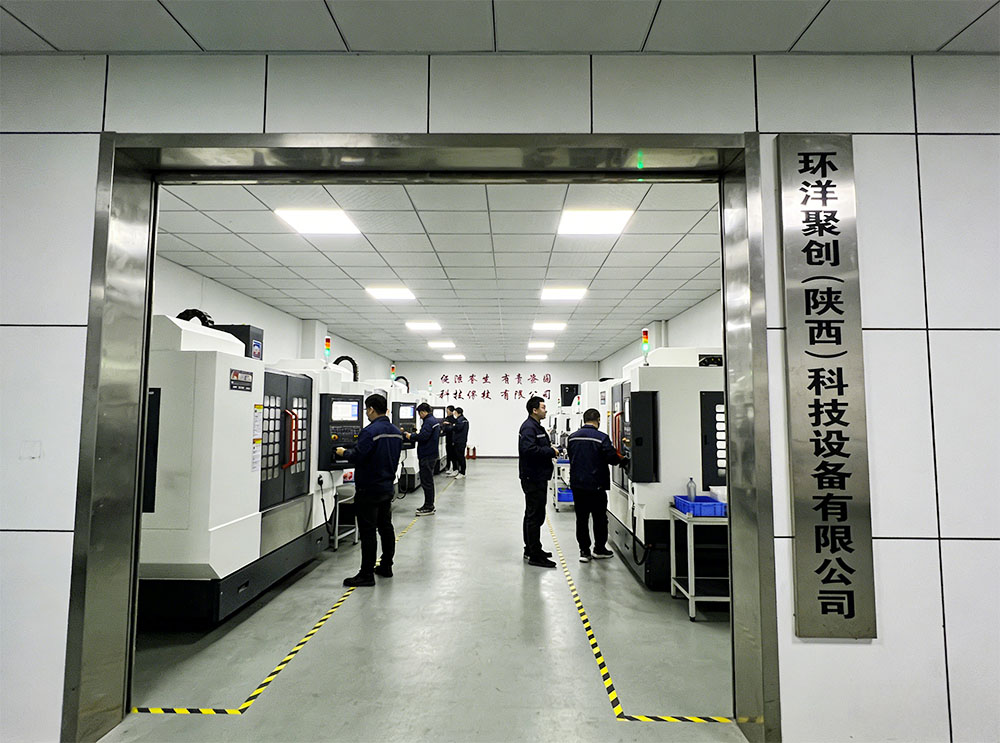
We have always adhered to the "people-oriented" principle, paid attention to the protection of employees' rights and interests, built a warm and cohesive team, and allowed every employee to exert their value in their positions.
Talent Philosophy: Respect talents, cultivate talents, and achieve talents. Adhere to "matching people with positions and teaching students in accordance with their aptitude", providing each employee with a broad development platform and growth space.
Team Building: Regularly carry out professional skills training, industry exchanges and team building activities to improve professional quality and collaboration ability; establish a sound performance appraisal and incentive mechanism to fully mobilize the enthusiasm and creativity of employees.
Core Team: All core members have more than 10 years of industry experience, with profound industry insight, rich practical experience and strong execution ability — accurately grasping industry development trends and quickly responding to market demands.
Huanyang Juchuang has formed four core advantages that build irreplaceable industry competitiveness.
As the only professional service provider in China with full-category and full-scenario parts coverage, our products cover four major fields: buses, agricultural machinery, commercial vehicles and mining equipment — eliminating the trouble of multi-channel procurement.
We have a mature R&D team and a complete R&D system, with strong customized R&D capabilities. Relying on profound technical reserves, we ensure stable product quality and strong adaptability, effectively reducing equipment failures.
We have built a first-class supply chain integration system, integrating high-quality upstream and downstream resources, realizing integrated management of procurement, production, warehousing and distribution with a complete nationwide logistics network.
We have a professional, efficient and fast-response service team providing full-process service from consultation and product selection to after-sales maintenance — one-on-one exclusive services that let customers have no worries.
Among numerous equipment parts service providers, Huanyang Juchuang has become the preferred partner of customers across the country with unique advantages and sincere services.
Products have passed strict testing with stable quality and strong adaptability. A complete quality control system prevents unqualified products from entering the market.
Full-category and full-scenario parts coverage enables one-stop procurement, saving time and costs while improving efficiency.
Our strong R&D team customizes exclusive parts solutions for special needs, solving personalized and difficult problems efficiently.
Nationwide coverage across 32 provinces with one-on-one exclusive services, quick response, timely delivery and effective after-sales support.
Honest operation principles and a commitment to mutual benefit have earned long-term trust and stable cooperative relationships with customers nationwide.
The only professional service provider in China achieving full-category and full-scenario parts coverage — a recognized benchmark in the equipment parts industry.
Explore our extended range of precision oil and air filter products for agricultural machinery, commercial vehicles, mining equipment and bus applications.
Huanyang Juchuang — Building quality with professionalism, winning trust with service, and leading the future with innovation. We are willing to work hand in hand with partners from all walks of life to build a new brilliance of the industry and contribute to the high-quality development of the equipment parts field.
