
Leave Your Message
-
Phone
-
E-mail
-
Whatsapp

-
Whatsapp

Explore our premium range of heavy-duty oil pumps and specialized air filtration kits engineered for maximum equipment lifecycle.


When discussing internal combustion engine health, standard oil filters and air filters are typically categorized as separate systems. However, in heavy-duty commercial vehicles, mining machinery, and agricultural tractors, the crossover between oil filtration and intake air filtration is critical. The concept of an oil filter for vehicle intake air filtration primarily refers to two vital technologies: oil bath air filters (which use an oil reservoir to capture airborne particles) and the critical coordination between oil mist separators and intake lines to prevent engine contamination. For heavy-duty machinery operating in high-dust environments, clean intake air is the single most important factor determining engine longevity.
Modern industrial operations face unprecedented demands for efficiency and uptime. In mining sectors, massive dump trucks like the Belaz 7555 or Belaz 7560 operate in continuous 24-hour cycles surrounded by highly abrasive particulate matter. Standard dry paper air filters in these environments can clog within hours, leading to severe air restriction, reduced fuel economy, and premature engine wear. Consequently, industrial operators rely on multi-stage filtration systems that combine oil-wetted technologies, centrifugal pre-cleaners, and heavy-duty oil pumps to maintain optimal engine breathing and lubrication. The global market for heavy-duty vehicle intake air filtration is shifting rapidly toward hybrid systems that integrate smart sensor monitoring with highly durable, cleanable oil-bath or oil-wetted elements to minimize waste and reduce operating expenses (OPEX).
By capturing 99.9% of micro-particles before they reach the combustion chamber, high-performance oil and air filtration systems prevent cylinder wall scoring and piston ring degradation.
Longer filter service intervals mean fewer replacements, lower maintenance labor costs, and significantly decreased vehicle downtime in critical mining and farming operations.
Unrestricted, clean air intake ensures an optimal air-fuel ratio, allowing high-displacement diesel engines to operate at peak thermal efficiency and lower emission levels.
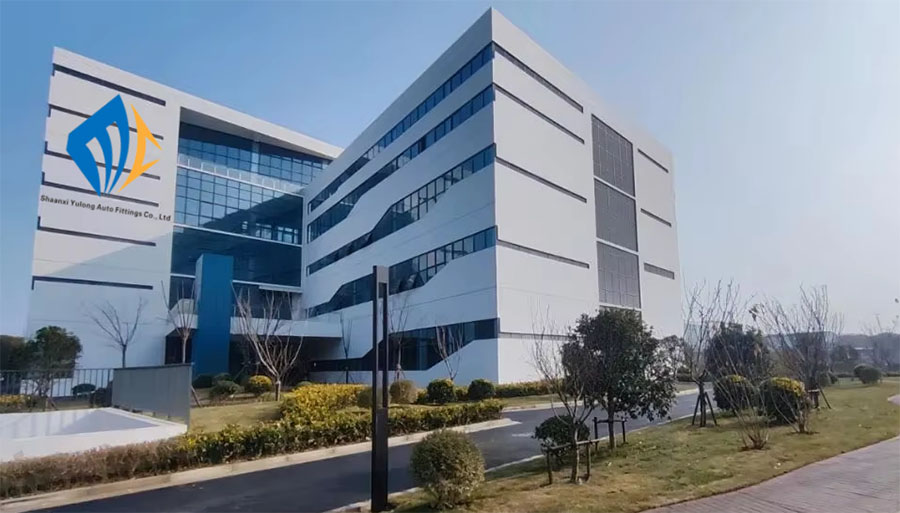
Huanyang Juchuang (Shaanxi) Technology Equipment Co., Ltd.
Huanyang Juchuang (Shaanxi) Technology Equipment Co., Ltd. is a professional and highly competitive leading enterprise in the field of parts for buses, agricultural machinery, commercial vehicles, and mining equipment. With years of in-depth cultivation in the industry, we have always adhered to the core philosophy of "Professionalism Builds Quality, Innovation Leads the Future", and strived to become a benchmark enterprise in China's equipment parts industry. We provide full-chain, high-quality parts products and service solutions for customers in various industries, helping the industry develop efficiently and stably.
Our dedication to quality control and technical innovation ensures that every oil pump, air filter kit, and moisture-oil separator we supply meets or exceeds OEM specifications, offering unmatched reliability under the most demanding field conditions.
Mining environments are arguably the most punishing proving grounds for heavy-duty machinery. Massive dump trucks, powered by high-horsepower diesel engines, require thousands of cubic meters of clean air per hour. Here, the air intake system is constantly bombarded by silica dust, coal dust, and metallic particles. If these contaminants bypass the air filter, they mix with the engine oil, turning the lubricant into an abrasive grinding paste. This is where components like the Belaz Front Oil Pump Assembly and specialized oil-separators play a crucial role. A robust oil pump ensures that even if micro-particles enter the lubrication cycle, they are quickly pushed through high-efficiency oil filters before causing bearing failure. Furthermore, moisture-oil separators with RDV valves prevent water vapor and blow-by oil mist from re-entering the intake manifold, preventing carbon buildup on intake valves.
In agriculture, harvesting operations generate thick clouds of dry organic dust, chaff, and soil particles. Tractors like the John Deere 6105M and 6140M require specialized multi-stage air filter kits (such as the AL115625 and AL177185) that utilize pre-cleaners to spin out heavy debris, followed by primary and safety elements to capture fine particles. In older or highly specialized agricultural setups, oil bath air filters are still utilized due to their ability to hold massive amounts of dust without a drop in static pressure. Modern tractors also leverage advanced oil filters to keep the engine oil clean as it lubricates turbocharger bearings, which are highly sensitive to intake-derived contaminants.
For commercial transport trucks (Freightliner, International, Kenworth, Peterbilt powered by Cummins engines), fuel economy and uptime are the primary drivers of profitability. These vehicles utilize high-capacity oil filters like the LF3000 / XLF75000 to maintain oil purity over extended drain intervals (often exceeding 50,000 miles). Clean oil directly affects the efficiency of variable valve timing and turbocharger actuators, which are linked to the overall air intake and exhaust gas recirculation (EGR) systems. Keeping both the air intake and oil filtration systems in perfect harmony prevents the formation of sludge and varnishes within the engine block.
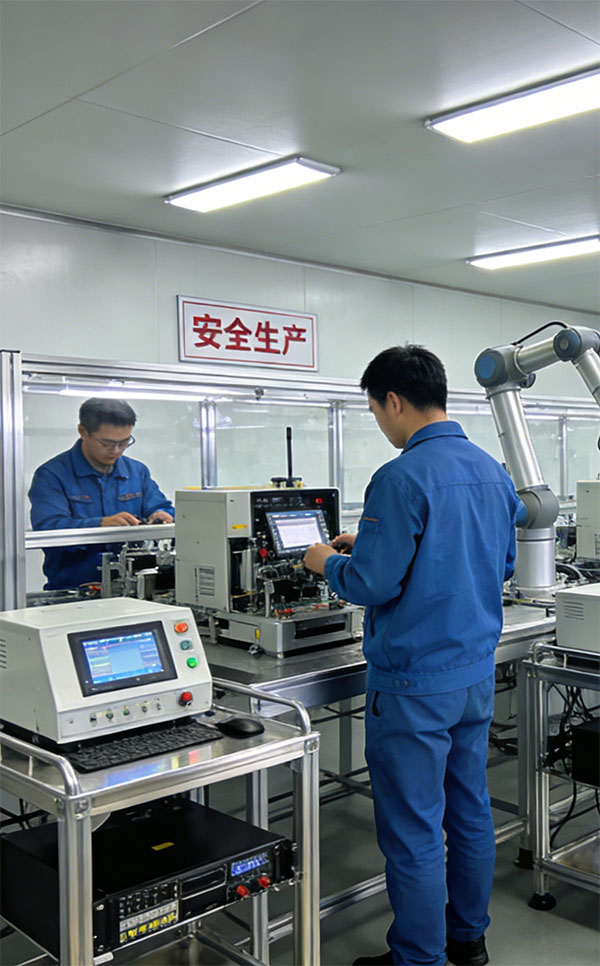
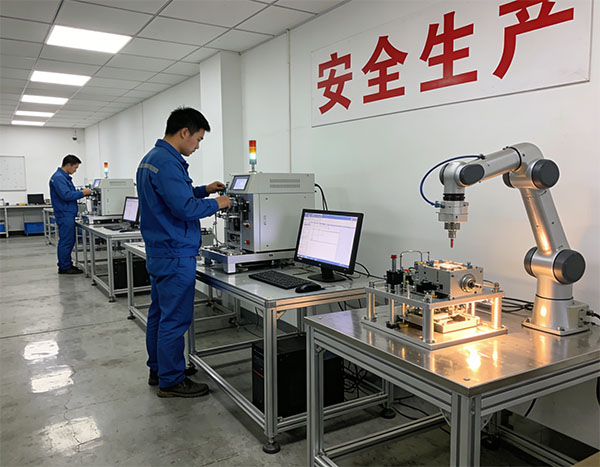
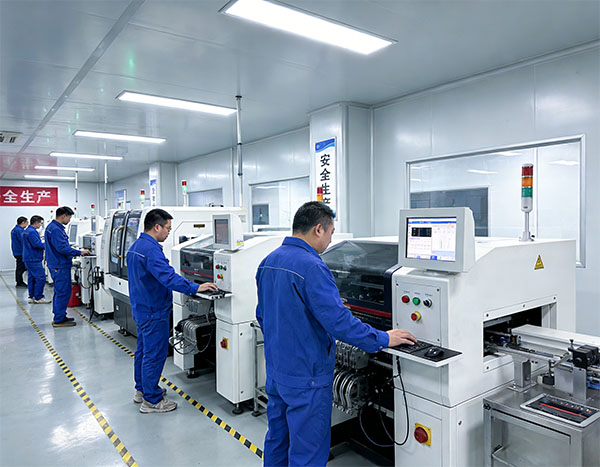
Comprehensive Parts Solutions for Heavy-Duty Sectors
Since its establishment, Huanyang Juchuang has adhered to the principles of honest operation and pragmatic practice. Relying on profound industry accumulation, mature technical strength, and a complete service system, we have won high recognition and trust from customers in 32 provinces, autonomous regions, and municipalities directly under the Central Government of China. We have gradually developed into a comprehensive parts service provider integrating R&D, production, integrated supply, and sales, and are currently a leading professional service provider in China that has achieved full-category and full-scenario parts coverage.
The heavy machinery industry is undergoing a massive shift toward sustainability, reduced carbon footprints, and predictive maintenance. Filtration systems, being the first line of defense for internal combustion engines, are at the forefront of this evolution. Here are the key trends shaping the future of vehicle intake air and oil filtration:
Traditional filter maintenance relies on fixed schedules or basic mechanical restriction indicators. Next-generation filtration systems integrate electronic differential pressure sensors directly into the vehicle's telematics network. These sensors monitor air restriction and oil contamination levels in real-time, predicting exactly when a filter will reach its holding capacity. This prevents premature replacement (saving costs) and guards against catastrophic failure from overloaded filters.
Standard cellulose (paper) filter media is increasingly being replaced by synthetic nanofibers. Nanofiber membranes feature much smaller pore sizes while maintaining high air permeability. This allows the filter to capture sub-micron soot and dust particles that would normally pass through standard filters or clog them rapidly. When paired with high-performance oil filters (like the LF3000 series), nanofiber intake filters ensure that the combustion chamber remains virtually sterile, drastically reducing engine wear rates.
Environmental regulations are pushing manufacturers to design filters with lower environmental impacts. This has led to the revival and modernization of high-efficiency cleanable elements and the use of metal-free, incinerable "eco" filter cartridges. By eliminating metal endcaps and center tubes, these filters reduce the volume of hazardous waste sent to landfills during routine maintenance cycles.
The company started in the field of equipment parts trade. With accurate industry insight and an honest business philosophy, it quickly opened up the domestic market and accumulated a large number of high-quality customer resources and industry experience. With the upgrading of market demand, the company gradually expanded its business boundaries, set up a professional R&D team, invested in production line construction, and realized the transformation from a "trading-oriented" enterprise to an integrated "R&D, production + trade and service" enterprise.
In the process of development, we have always adhered to the parallel development of technological innovation and service upgrading, continuously optimized the product system, improved the supply chain layout, and gradually expanded the coverage of the sales network to achieve full coverage in 32 provinces, autonomous regions, and municipalities in China.
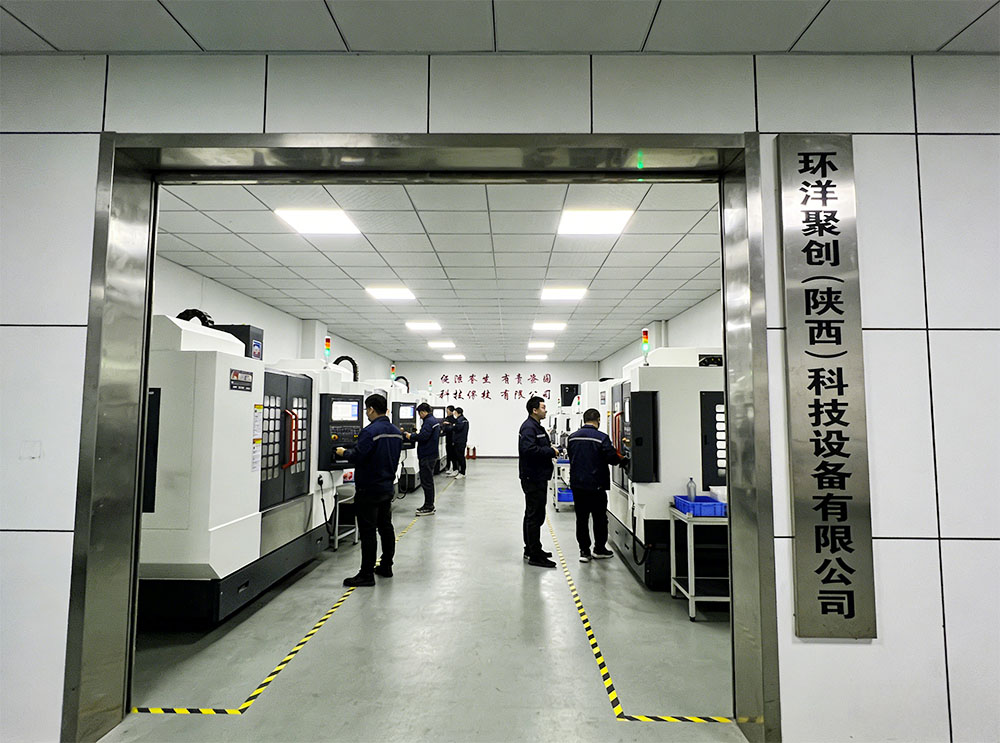
People-Oriented, Professional, and Highly Cohesive
The team is the core competitiveness of the enterprise. Huanyang Juchuang has always attached great importance to talent training and team building, and has built a core team that is "professional, efficient, pragmatic and innovative", covering various fields such as R&D, production, sales, service, and management.
Building irreplaceable industry competitiveness through years of in-depth cultivation and continuous investment.
Discover the core reasons why clients nationwide choose Huanyang Juchuang as their trusted parts partner.
A glimpse into our manufacturing, warehousing, and quality control departments.
Browse our complete list of premium heavy-duty engine parts, filtration systems, and oil pump assemblies.
