Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
Whatsapp
Precision-engineered vehicle cabin air filters designed for regular automotive maintenance across heavy-duty and commercial applications.

A vehicle cabin air filter is a critical component of any automotive HVAC (heating, ventilation, and air conditioning) system. Positioned in the air intake pathway, it captures airborne contaminants — including dust, pollen, mold spores, bacteria, exhaust gases, and fine particulate matter (PM2.5) — before they enter the vehicle's passenger or operator compartment. For drivers and operators spending extended hours inside buses, agricultural tractors, mining dump trucks, or commercial freight vehicles, a clean and fully functional cabin air filter is not a luxury but an occupational health necessity.
Regular automotive maintenance schedules universally recommend cabin air filter inspection and replacement at intervals ranging from every 15,000 to 25,000 kilometers, or at least once per year under normal operating conditions. In high-dust environments — such as open-pit mining sites, agricultural fields during harvest, or urban construction zones — replacement intervals should be significantly shortened to maintain optimal filtration efficiency and prevent HVAC system strain.
Studies indicate that the air inside a vehicle cabin can be up to 6× more polluted than the air outside when the cabin filter is clogged or absent. For operators of mining equipment and agricultural machinery working in dust-heavy environments, this risk is dramatically amplified, making routine cabin air filter maintenance an essential occupational safety measure.
The global automotive cabin air filter market has experienced robust growth over the past decade, driven by rising awareness of indoor air quality, stricter occupational health regulations, and the rapid expansion of commercial vehicle fleets worldwide. According to industry analysis, the global cabin air filter market was valued at approximately USD 4.2 billion in 2023 and is projected to surpass USD 6.8 billion by 2030, growing at a CAGR of around 7.1%.
Within China — the world's largest automotive market — the demand for cabin air filters in commercial and industrial segments has grown particularly fast. The agricultural mechanization drive, expansion of urban bus transit networks, and the boom in large-scale mining operations across Inner Mongolia, Xinjiang, and Shanxi have all created sustained, high-volume demand for quality cabin filtration products. Enterprises like Huanyang Juchuang (Shaanxi) Technology Equipment Co., Ltd. have emerged as key players, offering full-category, full-scenario parts coverage specifically tailored to these demanding industrial applications.
Traditional paper-based cabin filters are rapidly being supplemented or replaced by multi-layer composite filters incorporating electrostatic media, activated carbon layers, and HEPA-grade materials. These advanced filters can capture particles as small as 0.3 microns with efficiency rates exceeding 99.97%, providing superior protection for operators in high-pollution environments such as mining sites and industrial agricultural zones.
The integration of IoT-enabled filter condition sensors into commercial vehicle and heavy equipment management systems represents a significant emerging trend. These systems provide real-time data on filter loading status, alerting fleet managers when replacement is due, thereby eliminating guesswork from maintenance schedules and reducing both under-maintenance risks and unnecessary early replacements. This development is closely aligned with the broader Industry 4.0 transformation of fleet maintenance management.
Environmental regulations are pushing manufacturers toward more sustainable filter media and packaging. Biodegradable filter frames, recyclable filter media, and low-emission manufacturing processes are increasingly becoming standard requirements in procurement specifications for large commercial fleet operators and government-run transit agencies.
Leading parts suppliers are moving beyond generic fitment toward highly customized, OEM-specification cabin air filters designed for specific vehicle models and operating environments. For specialized equipment like the John Deere 6105M–6140M agricultural tractor series or the BelAZ 7513/75131/75135 mining dump trucks, precision-fit filter kits ensure optimal sealing, maximum filtration surface area, and compatibility with the vehicle's HVAC architecture.
Mining dump trucks operating in open-pit environments face some of the most extreme cabin air filtration challenges of any vehicle type. Dust concentrations on active mining haul roads can exceed 10 mg/m³ — more than 10× the occupational exposure limit. High-capacity cabin air filter kits with extended service intervals and dust-loading capacity are critical for protecting operators and maintaining equipment HVAC performance in these conditions.
During peak harvest operations, agricultural tractors, combine harvesters, and sprayers operate in environments with extremely high concentrations of crop dust, pollen, pesticide aerosols, and soil particles. Cabin air filters in agricultural equipment must handle these mixed contaminant profiles while maintaining adequate airflow for operator comfort in hot, humid conditions. Multi-layer filters combining mechanical filtration with activated carbon odor adsorption are the preferred specification for this application segment. Products like the AL115625 / AL177185 Air Filter Kit for John Deere 6105M–6140M are engineered specifically for these demanding agricultural operating conditions.
For long-haul trucking fleets and urban delivery vehicle operators, cabin air filter maintenance is a key component of total fleet cost management. A clogged cabin filter increases the load on the HVAC blower motor, raises fuel consumption for climate control, and degrades driver comfort — all of which impact operational efficiency. Fleet operators are increasingly adopting predictive maintenance models that incorporate cabin filter condition monitoring alongside engine air filter and oil change intervals to optimize total maintenance cost per kilometer.
Public transit buses carry hundreds of passengers daily through urban environments with elevated levels of traffic-related air pollution. Regulatory frameworks in many jurisdictions now mandate minimum cabin air quality standards for public transport vehicles, requiring certified-performance cabin air filters with documented replacement schedules. This regulatory pressure is driving significant procurement activity for high-performance cabin filtration systems across municipal bus fleets worldwide.
The BelAZ 7513 series — among the world's largest mining dump trucks — operates in conditions that challenge every component of the vehicle's systems. Cabin air filtration for these machines must deliver reliable protection against silica dust, diesel exhaust particulates, and explosive-site chemical vapors, while maintaining performance across extreme temperature ranges from -40°C in Siberian winter conditions to +45°C in desert open-pit environments. Precision-engineered cabin filter assemblies, such as the BelAZ 7513 / 75131 / 75135 series components, are essential maintenance items for keeping operators safe and equipment operational.
Effective cabin air filter maintenance within a regular automotive maintenance program involves more than simply replacing the filter at scheduled intervals. Best practices for commercial and industrial fleet operators include: establishing environment-specific replacement intervals (shorter in high-dust conditions); inspecting filter condition at every major service event; using OEM-specification or certified-equivalent filters to ensure proper fit and filtration performance; documenting filter replacements as part of the vehicle service record; and training maintenance personnel to recognize the signs of filter bypass or seal failure that can compromise filtration effectiveness even with a new filter installed.
Filters out PM2.5, pollen, bacteria and chemical vapors that cause respiratory illness and reduce operator alertness in long-shift operations.
A clean cabin filter reduces blower motor load, improving A/C and heating performance while lowering energy consumption and component wear.
Reduced HVAC system strain translates to measurable fuel savings — particularly significant for high-utilization commercial vehicles and mining equipment.
Meets occupational health standards and transit authority air quality regulations, protecting operators and fleet operators from regulatory liability.
Prevents dust ingress into HVAC evaporator and heater core components, significantly extending the service life of expensive climate control hardware.
Integration with smart monitoring systems enables data-driven maintenance scheduling, reducing unplanned downtime and optimizing total fleet maintenance costs.
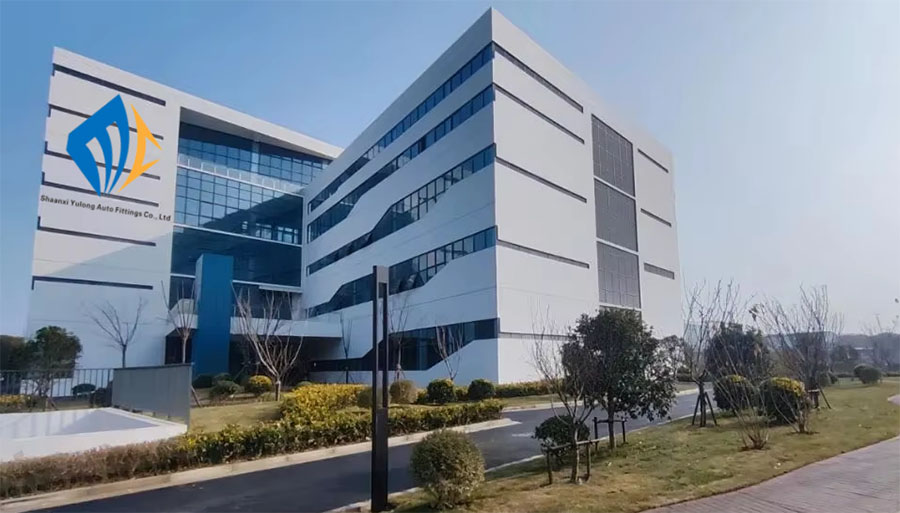
Huanyang Juchuang (Shaanxi) Technology Equipment Co., Ltd. is a professional and highly competitive leading enterprise in the field of parts for buses, agricultural machinery, commercial vehicles and mining equipment. With years of in-depth cultivation in the industry, we have always adhered to the core philosophy of "Professionalism Builds Quality, Innovation Leads the Future", and strived to become a benchmark enterprise in China's equipment parts industry.
Since its establishment, the company has adhered to the principles of honest operation and pragmatic practice. Relying on profound industry accumulation, mature technical strength and a complete service system, it has won high recognition and trust from customers in 32 provinces, autonomous regions and municipalities directly under the Central Government of China.
We provide full-chain, high-quality parts products and service solutions for customers in various industries, helping the industry develop efficiently and stably.
Focused on four major fields with a complete, full-scenario parts supply system — from cabin air filters to core transmission and structural components.
The company focuses on the R&D, production, integrated supply and sales of parts in four major fields: buses, agricultural machinery, commercial vehicles and mining equipment. Core business covers customized R&D, standardized production, batch supply and supporting services of all major equipment parts.
Our product system covers all categories and scenarios from core transmission components and braking components to general electrical accessories, structural parts, and cabin air filtration systems — meeting the personalized needs of different customers.
Relying on a professional technical team, we provide timely, customized and one-stop overall parts solutions for mining dump truck and heavy equipment users, solving the pain points of scattered procurement, poor adaptability and delayed supply.
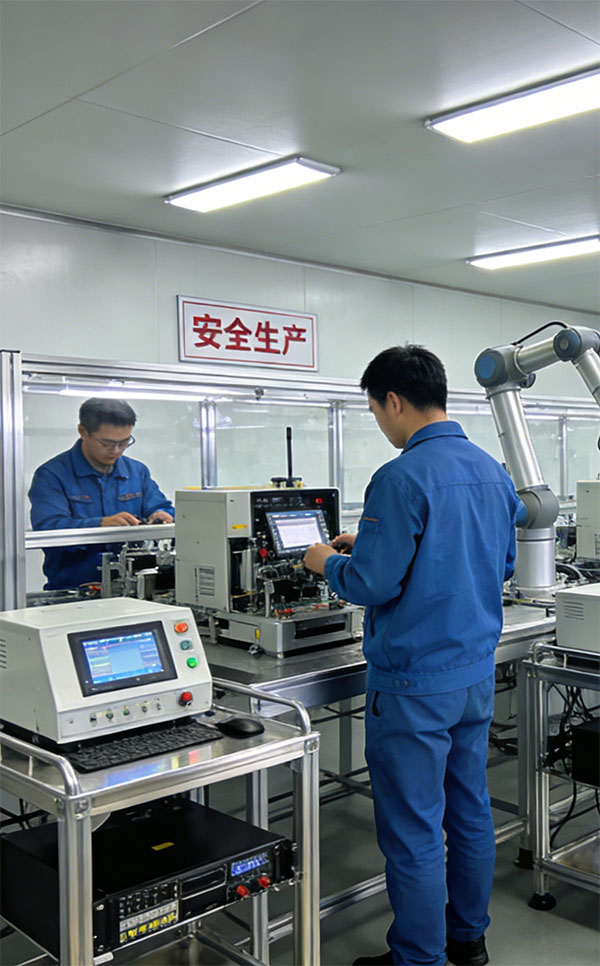
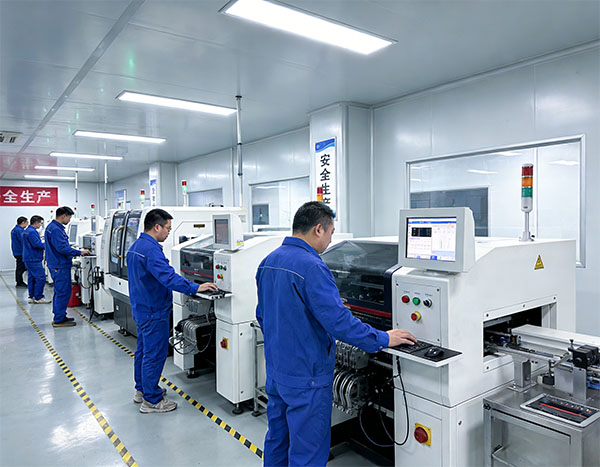
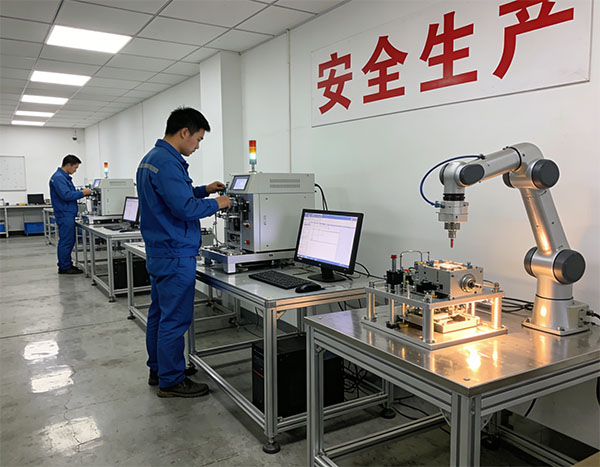
Relying on years of in-depth industry cultivation and continuous investment, Huanyang Juchuang has formed four core advantages that build irreplaceable industry competitiveness.
As the only professional service provider in China with full-category and full-scenario parts coverage, our products cover four major fields: buses, agricultural machinery, commercial vehicles and mining equipment. Complete categories and various specifications eliminate the trouble of multi-channel procurement and greatly improve customer procurement efficiency.
We have a mature R&D team and a complete R&D system, with strong customized R&D capabilities and technical upgrading capabilities. Relying on profound technical reserves, we ensure stable product quality and strong adaptability, effectively reducing equipment failures and ensuring efficient operation.
We have built a first-class supply chain integration system, integrating high-quality upstream and downstream resources, realizing integrated management of procurement, production, warehousing and distribution. We can quickly respond to the needs of customers across the country, ensuring timely and safe delivery of parts.
We have a professional, efficient and fast-response service team with a full-process service system. From customer consultation, product selection, customized solutions to after-sales maintenance and parts supply, we provide one-on-one exclusive services that let customers have no worries.
The company started in the field of equipment parts trade. With accurate industry insight and honest business philosophy, it quickly opened up the domestic market and accumulated a large number of high-quality customer resources and industry experience. With the upgrading of market demand, the company gradually expanded its business boundaries, set up a professional R&D team, invested in production line construction, and realized the transformation from a "trading-oriented" enterprise to an integrated "R&D, production + trade and service" enterprise.
In the process of development, we have always adhered to the parallel development of technological innovation and service upgrading, continuously optimized the product system, improved the supply chain layout, and gradually expanded the coverage of the sales network to achieve full coverage in 32 provinces, autonomous regions and municipalities directly under the Central Government of China.
After years of in-depth cultivation, the company has successfully broken through technical bottlenecks, built a full-category parts supply system, become the only professional service provider in China that achieves full-category and full-scenario parts coverage, and established a solid brand reputation and professional benchmark in the industry.
In the future, the company will continue to deepen its focus on core fields, expand product application scenarios, promote technological iteration and upgrading, and steadily move towards the goal of "building a leading domestic and internationally renowned equipment parts service provider".
Products pass strict testing with stable quality and strong adaptability. Complete quality control system prevents unqualified products from entering the market.
One-stop parts coverage saves multi-channel procurement trouble, reducing procurement time and costs while improving efficiency.
Strong R&D team customizes exclusive parts solutions for special needs, solving personalized and difficult problems to upgrade equipment performance.
Sales and service network covering 32 provinces, with one-on-one exclusive service, quick response, timely delivery and after-sales support.
Honest operation philosophy, respecting customers and valuing customer interests. Long-term cooperative relationships built on mutual benefit and common development.
Continuously promoting technological iteration and upgrading, expanding product application scenarios, and steadily advancing toward international recognition.
Corporate culture is the core driving force for enterprise development. Huanyang Juchuang has always adhered to the core values of "Integrity, Professionalism, Innovation and Win-Win", integrating corporate culture into every link of production, R&D, sales and service.
Integrity as the foundation, professionalism as the foundation, innovation for the future, and win-win coexistence
Empower equipment upgrading with high-quality parts, assist customer development with professional services, and promote high-quality progress of the industry
Become a benchmark enterprise in China's equipment parts industry and build a sustainable and win-win industrial ecosystem
Pragmatic practice, striving for excellence, forging ahead with determination, and climbing new heights
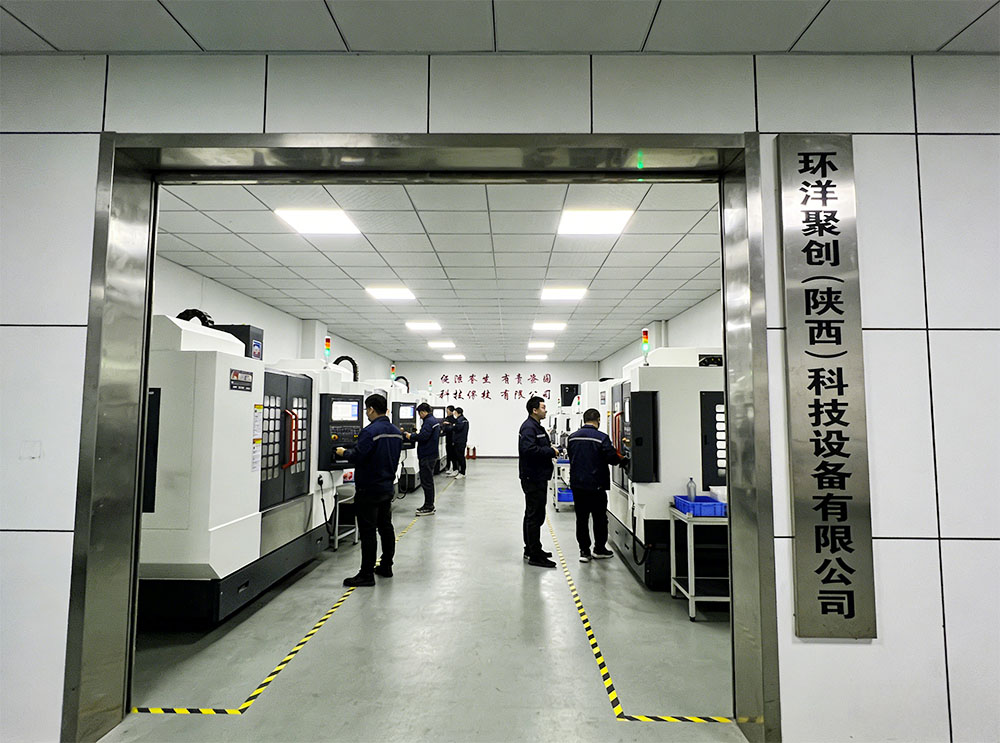
The team is the core competitiveness of the enterprise. Huanyang Juchuang has always attached great importance to talent training and team building, and has built a core team that is "professional, efficient, pragmatic and innovative", covering various fields such as R&D, production, sales, service and management.
Talent Philosophy: Respect talents, cultivate talents, and achieve talents. Adhere to "matching people with positions and teaching students in accordance with their aptitude", providing each employee with a broad development platform and growth space, and realizing the common growth of employees and the enterprise.
Team Building: Regularly carry out professional skills training, industry exchanges and team building activities to improve the professional quality and collaboration ability of the team; establish a sound performance appraisal and incentive mechanism to fully mobilize the enthusiasm and creativity of employees.
Core Team: All core members have more than 10 years of industry experience, with profound industry insight, rich practical experience and strong execution ability. They can accurately grasp the development trend of the industry, quickly respond to market demand, and lead the enterprise to move forward steadily.
Explore our comprehensive range of vehicle cabin air filters and regular automotive maintenance components for all major equipment categories.